


How to Choose a Hot Extrusion Hydraulic Press Line in 2026?
Choosing a Hot Extrusion Hydraulic Press Line in 2026 requires more than comparing tonnage and purchase prices. The right line must match your alloy, billet diameter, profile size, production volume, and available floor space. It should also support stable pressure control, accurate temperature management, efficient cooling, and safe maintenance access. A powerful press can still produce inconsistent profiles when tooling, billet heating, and speed control are poorly matched.
Dr. J. G. Lenard, a respected extrusion researcher and author, stated, “Extrusion is a metal forming process in which a billet is forced through a die.” That simple principle carries serious purchasing consequences. The die, container, stem, and hydraulic system must work as one system. Look closely at cycle time, maximum extrusion force, oil filtration, pump response, energy consumption, and spare-parts availability. Ask the supplier for comparable installation data, not only polished showroom samples. Request details about actual alloy grades and profile dimensions.
Small details matter.
A practical evaluation should include factory acceptance testing, operator training, remote diagnostics, and documented service response times. Check whether the control system can record pressure curves and temperature changes. These records help identify defects before they become expensive batches. I would not choose the cheapest line automatically. Nor would I assume the largest press is the safest investment. Some buyers overlook foundation loads and later discover costly installation problems. A careful decision leaves room for uncertainty, because real production rarely behaves exactly like a brochure.
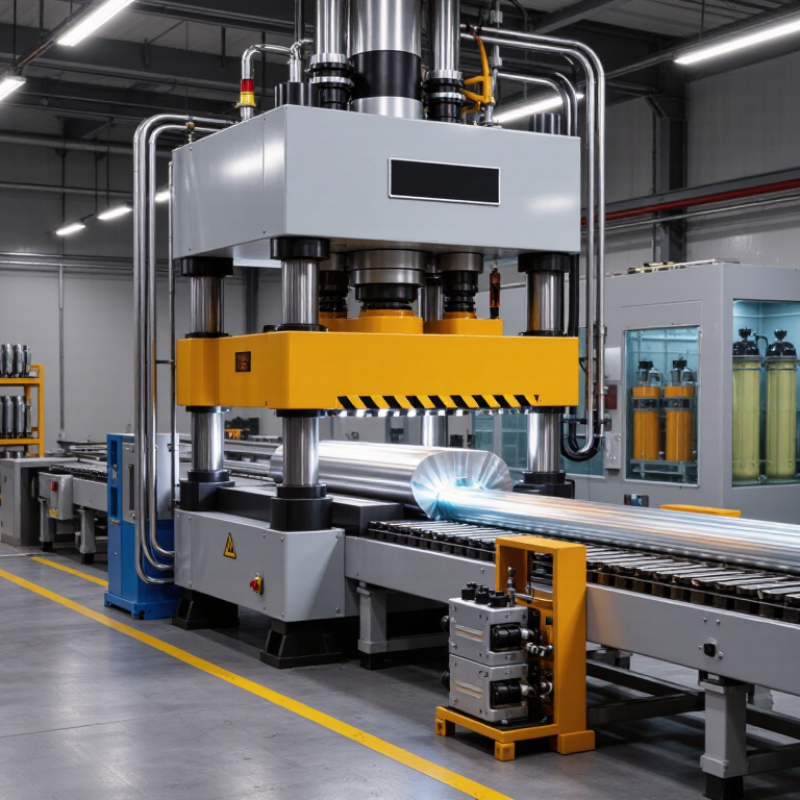
Define the Products, Materials, and Production Requirements
How to Choose a Hot Extrusion Hydraulic Press Line in 2026?
Define the product before comparing press capacities. Record profile shape, cross-sectional area, length, tolerance, surface finish, and expected scrap rate. A thin architectural profile needs different control from a thick structural section. Check the extrusion ratio, billet diameter, container size, and required ram force together. Do not select tonnage from product weight alone.
Materials change the process window. Aluminium alloys require controlled billet heating, stable die temperatures, and reliable quenching. The International Aluminium Institute reported approximately 72.8 million tonnes of global primary aluminium production in 2024, showing the scale of this market. Steel and copper demand higher forming forces and more severe tooling conditions. The World Steel Association reported about 1.84 billion tonnes of crude steel production in 2024. These figures support careful material planning, not automatic equipment selection.
Production requirements must be measurable. Define annual output, shifts, target cycle time, changeover frequency, and acceptable downtime. Specify the full route: billet heater, press, puller, quench, stretcher, saw, and aging system. Ask for force stability, temperature uniformity, energy consumption, and maintenance access. A line rated for maximum force may still miss your real throughput target. I have seen specifications focus on tonnage while ignoring die changes and cooling delays. That is an expensive oversight. Leave room for future alloys and longer profiles, but avoid buying unused capacity without a verified production forecast.
How to Choose a Hot Extrusion Hydraulic Press Line in 2026? - Define the Products, Materials, and Production Requirements
| Decision Dimension | Typical Requirement | Recommended Press-Line Specification | Why It Matters | 2026 Selection Checkpoint |
|---|---|---|---|---|
| Product Type | Solid round bars, square bars, or simple profiles | Direct hot extrusion press with billet container and die stack | Simple geometries generally require lower die complexity and shorter setup time. | Confirm the required diameter or across-flats range and acceptable dimensional tolerance. |
| Product Type | Hollow tubes and seamless tubular components | Piercing-capable extrusion line with mandrel or piercing tooling | Tube production adds piercing force, mandrel alignment, and wall-thickness control requirements. | Specify outside diameter, inside diameter, wall thickness, length, and concentricity target. |
| Product Type | Complex aluminum profiles for construction or transport applications | Indirect or direct extrusion press with automatic billet loading, die handling, run-out table, and puller | Profile complexity and surface quality depend on stable metal flow and controlled handling after extrusion. | Evaluate profile envelope, thin-wall sections, die diameter, and required straightness. |
| Material Family | Aluminum alloys, including common wrought grades | Approximately 10–35 MN press capacity for many commercial profile and bar applications | Aluminum normally requires lower extrusion force than steel and supports higher production speeds. | Match billet diameter, alloy flow stress, extrusion ratio, ram speed, and thermal-control capability. |
| Material Family | Copper and copper alloys for rods, tubes, and electrical components | Approximately 20–50 MN press capacity, with rigid tooling and controlled billet heating | Copper alloys demand high structural rigidity, accurate temperature control, and appropriate lubrication. | Verify alloy-specific temperature range, oxidation control, die life, and electrical-surface requirements. |
| Material Family | Carbon steel and low-alloy steel products | Approximately 50–150 MN press capacity, with high-temperature billet furnace and robust tooling | Steel extrusion requires much higher force, stronger tooling, and tighter thermal management than aluminum. | Check billet temperature, container strength, die material, press stroke, and cooling strategy. |
| Billet Diameter | Small and medium billets for flexible product families | Billet diameter commonly selected within approximately 100–250 mm, depending on material and product size | Billet size influences press force, product cross-section, yield, and the available extrusion ratio. | Choose a billet range that covers current products without creating excessive trimming or discard. |
| Required Capacity | Force requirement calculated from material strength, billet size, die geometry, and friction | Select rated capacity with a practical operating margin rather than sizing only to the average force | Insufficient capacity causes overloads, unstable extrusion, premature wear, and limited product flexibility. | Use verified force calculations and include peak-load conditions, not only nominal production data. |
| Production Volume | Single-shift or low-volume production | Semi-automatic line with manual die change and programmable press controls | Lower automation reduces initial complexity while retaining repeatable process control. | Prioritize simple maintenance, quick access to wear parts, and future automation compatibility. |
| Production Volume | Continuous, multi-shift production with high equipment utilization | Fully integrated line with billet loader, automatic heating, die handling, puller, cooling, cutting, and data monitoring | Automation reduces handling time, improves consistency, and supports predictable cycle times. | Compare OEE targets, changeover time, planned maintenance hours, and spare-part availability. |
| Extrusion Speed | Moderate speed for general-purpose bars and profiles | Adjustable ram speed with closed-loop hydraulic control and recipe storage | Controlled speed helps balance productivity, surface finish, dimensional accuracy, and die temperature. | Request speed ranges for each alloy and product rather than relying on one maximum-speed value. |
| Heating System | Uniform billet heating before extrusion | Gas or induction heating selected according to billet material, diameter, throughput, and energy strategy | Temperature uniformity directly affects flow behavior, surface quality, die wear, and energy use. | Specify temperature uniformity, heating rate, furnace capacity, insulation, and emissions requirements. |
| Dimensional Quality | Tight profile dimensions and repeatable surface finish | Rigid frame, accurate guide system, stable hydraulic pressure, die preheating, and inline measurement where required | Mechanical deflection, temperature variation, and pressure fluctuation can create dimensional drift. | Define tolerances using applicable product standards and validate them through a production trial. |
| Energy and Sustainability | Lower energy consumption and reduced hydraulic heat generation | Variable-speed pump drives, efficient heaters, heat recovery options, and energy monitoring | Energy demand affects operating cost, cooling requirements, and long-term environmental performance. | Request energy consumption per tonne or per production cycle under defined operating conditions. |
| Control and Data | Traceable production parameters and predictive maintenance support | PLC-based control, HMI recipe management, alarm history, pressure and temperature logging, and industrial network connectivity | Process data helps identify defects, standardize recipes, and schedule maintenance before failures occur. | Confirm data ownership, export formats, cybersecurity controls, remote-access policy, and integration requirements. |
| Safety and Compliance | Protection from high pressure, hot billets, moving tooling, and stored hydraulic energy | Guarding, interlocks, emergency stops, pressure relief, safe maintenance access, and documented risk assessment | Hot extrusion combines high mechanical force and high temperature, requiring engineered safeguards. | Verify compliance with applicable local machinery, electrical, pressure, and workplace-safety requirements. |
| Factory Layout | Available floor space, crane capacity, utilities, ventilation, and material flow | Layout planned around press footprint, heating equipment, run-out table, cooling, saw, puller, and finished-product handling | Poor layout increases handling distance, installation cost, safety risk, and downtime. | Complete a utility and foundation survey before finalizing the press-line configuration. |
| Lifecycle Cost | Reliable output over a planned service life of approximately 10–20 years | Evaluate purchase price together with energy, tooling, labor, maintenance, consumables, downtime, and upgrades | The lowest initial price may result in higher operating cost or reduced production availability. | Use a total-cost-of-ownership model based on annual tonnes, shifts, energy price, and maintenance intervals. |