Biotech, pharma, food industries equipment & plants
Choosing the best Chamfering Cutter supplier in China requires more than comparing online prices. The decision affects edge quality, tool life, production speed, and the consistency of finished parts. In daily machining, a cutter may appear acceptable while leaving uneven edges or visible burrs after repeated use. Small errors can increase rework and waste valuable material. The right supplier should understand these practical risks. Yet price alone remains a common buying factor. That assumption deserves careful review.
A reliable evaluation begins with technical evidence. Ask about carbide grade, cutter geometry, coating options, dimensional tolerance, and compatible materials. Request inspection reports and sample specifications before placing a large order. Check whether the supplier controls runout, cutting-edge sharpness, and surface finish during production. Photos are useful, but physical samples provide stronger evidence. Testing several pieces on your own equipment can reveal vibration, heat buildup, and actual tool durability. This step connects supplier claims with manufacturing experience. Do not skip it.
Supplier communication also reveals professional reliability. Clear answers about lead times, packaging, replacements, and quality procedures indicate stronger internal control. A trustworthy company should explain limitations instead of promising perfect results. Still, no supplier is perfect. Some catalogs may contain outdated data, and even experienced buyers can overlook application details. A trial order can expose these weaknesses early. Keep records of test results, feedback, and repeat performance. This guide will examine how to compare Chinese suppliers, verify their expertise, and select a Chamfering Cutter partner that supports stable, measurable production.
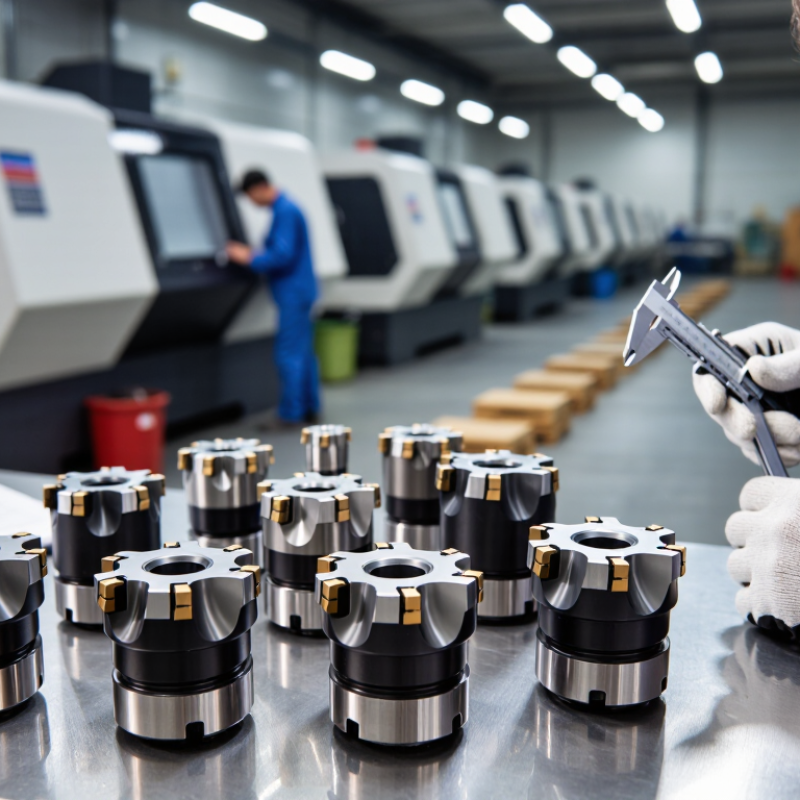
A chamfering cutter removes sharp edges and creates a clean angled surface on a workpiece. It may also prepare holes for screws, improve assembly, and reduce edge damage. Common types include countersink, carbide, and indexable cutters. Each design suits different materials, speeds, and production volumes.
Supplier selection matters because cutter quality affects accuracy, tool life, and surface finish. A reliable supplier should explain cutting geometry, coating options, tolerance limits, and recommended parameters. Ask for material certificates, inspection reports, and sample testing. A practical supplier will discuss your machine, workpiece material, and expected output instead of offering one universal solution. That detail shows technical experience.
Tips: Request a sample cutter before placing a large order. Check edge sharpness under good lighting. Measure the chamfer angle after machining. Review packaging, batch markings, and delivery records. Keep communication in writing. Small details matter.
Price still deserves attention. However, the cheapest cutter may create more rework and downtime. In my experience, supplier claims can sound precise but remain incomplete without test data. This is where careful comparison becomes important. Visit the factory online or in person when possible. Ask how workers inspect runout and edge geometry. A supplier that admits limitations may be more trustworthy than one promising perfect results every time. You should also confirm after-sales support, replacement policies, and response times before cooperation begins.
A reliable chamfering cutter starts with the workpiece, not the catalog photo. In practical machining, confirm the cutter material, cutting angle, diameter, shank size, and recommended speed range. Carbide suits hardened materials and longer production runs. High-speed steel may provide better flexibility for softer metals. The specified chamfer angle should match the drawing, commonly 45 degrees, but not always. Small errors become visible around holes and sharp edges.
Edge geometry also matters. Check the number of flutes, relief angle, rake angle, and chip-clearance design. More flutes can improve finish, but they may restrict chip evacuation in deep chamfers. A durable coating should match the material being cut and the coolant process. Coating alone does not prove quality. Ask for hardness data, coating type, and application guidance.
Dimensional control separates a dependable supplier from a promising one. Request shank tolerance, cutter diameter tolerance, concentricity, and runout data. Excessive runout can create uneven chamfers, vibration, and early edge failure. Inspection records should identify measuring equipment and batch numbers. A small sample test is still necessary. One cutter may perform well while another exposes inconsistency. I would also check edge sharpness under magnification and inspect the surface after several parts. Supplier experience helps, but clear specifications and traceable inspections deserve greater weight. No specification sheet removes every risk.
How to Choose the Best Chamfering Cutter Supplier in China?
A reliable supplier should prove quality through process control, not attractive photographs. Ask about carbide grade, coating options, edge preparation, and grinding accuracy. For chamfering cutters, inspect runout, cutting angle, surface finish, and dimensional consistency. A practical sample test can reveal problems quickly. Measure the cutter before and after machining. Check burr formation, tool wear, and hole-edge quality.
Manufacturing capability matters as much as product quality. Visit the factory when possible, or request a live video inspection. Look for modern CNC grinding machines, tool presetters, coating control, and clean inspection areas. Ask whether operators follow documented procedures. Request inspection reports, material certificates, and batch traceability. A supplier should explain how rejected tools are handled. Vague answers deserve caution. A polished website proves very little.
Tips: Compare samples from several suppliers. Use the same workpiece and cutting conditions. Ask for a tolerance chart, not only a promise. Confirm packaging, lead time, and replacement procedures in writing. Small details matter.
Experience also suggests leaving room for doubt. One excellent sample may not represent every batch. Repeated testing is safer. Suppliers can improve, but buyers must verify consistency. That extra inspection may feel slow. It often prevents expensive production interruptions.
| Evaluation Dimension | Recommended Benchmark | Evidence to Request | Suggested Scoring Method | Weight | Rating (1–5) |
|---|---|---|---|---|---|
| Product Specification Control | Published drawings should define cutter diameter, chamfer angle, cutting length, shank diameter, overall length, material, coating, and dimensional tolerances. | Controlled product drawings, revision history, inspection standards, and a completed sample inspection report. | 5 = complete, controlled documentation; 3 = partially documented; 1 = no controlled specification. | 15% | — |
| Raw Material Traceability | Each production lot should be traceable to the raw-material batch. Carbide or high-speed-steel certificates should identify grade, batch number, and supplier. | Material certificates, incoming inspection records, batch labels, and traceability procedures. EN 10204 Type 3.1 certificates may be requested where applicable. | 5 = complete lot traceability and certificates; 3 = partial records; 1 = undocumented material source. | 12% | — |
| Dimensional Accuracy | The supplier should demonstrate measurement capability for critical dimensions, including cutting diameter, shank diameter, chamfer angle, and overall length. Acceptance limits must be agreed on the drawing. | First-article inspection report, calibrated micrometers, optical measuring equipment, tool presetters, and measurement records linked to the production lot. | 5 = all critical dimensions meet agreed tolerances; 3 = minor variation requiring correction; 1 = repeated out-of-tolerance results. | 15% | — |
| Runout and Balance Control | For rotating tools, runout requirements should be specified according to tool diameter, holder system, spindle speed, and application. A practical sample target for precision small-diameter tools is often ≤0.02 mm at the specified inspection point, subject to drawing approval. | Runout test records, inspection setup details, dial indicators or optical systems, and sample test results at the required gauge length. | 5 = measured and consistently within agreed limit; 3 = measurement available but inconsistent; 1 = no runout control. | 12% | — |
| Grinding and Manufacturing Capability | The facility should have CNC tool-grinding equipment, suitable diamond grinding wheels, controlled coolant systems, and a documented setup process for repeat production. | Machine list, equipment maintenance records, process flow chart, production photographs or audit access, and sample capability-study results. | 5 = complete in-house process and stable repeatability; 3 = partial outsourcing; 1 = mainly trading or uncontrolled outsourcing. | 15% | — |
| Edge Quality and Surface Finish | Cutting edges should be free from harmful chips, cracks, excessive burrs, grinding burns, and coating defects. Surface-finish requirements should be defined for functional areas. | Microscope inspection images, edge-quality criteria, surface-finish records, nonconformance samples, and inspection frequency. | 5 = documented visual and microscopic inspection; 3 = basic visual inspection; 1 = no formal edge-quality criteria. | 10% | — |
| Coating and Post-Processing Control | If coated, the tool should have a defined coating type, intended workpiece material, application range, and coating-quality inspection method. Coating thickness and adhesion should be controlled according to the coating supplier’s technical specification. | Coating technical data sheet, lot certificate, coating inspection report, subcontractor controls, and coating defect criteria. | 5 = documented and lot-controlled coating process; 3 = certificate only; 1 = unspecified coating process. | 8% | — |
| Quality Management System | A documented quality management system should cover incoming inspection, process inspection, final inspection, corrective action, document control, and customer complaints. ISO 9001 certification is useful evidence but should not replace an audit. | Valid certificate, certification scope, internal audit records, corrective-action reports, control plans, and inspection procedures. | 5 = certified and effectively implemented; 3 = documented but weakly implemented; 1 = informal quality control. | 8% | — |
| Testing and Application Validation | Performance should be validated using the intended workpiece material, machine, spindle speed, feed rate, depth of cut, and coolant conditions. One universal cutting-speed value is not suitable for every application. | Application test report, recommended cutting parameters, tool-life results, workpiece samples or photographs, and failure-analysis records. | 5 = application-specific testing with repeatable results; 3 = basic sample testing; 1 = only catalog claims. | 8% | — |
| Capacity and Delivery Reliability | The supplier should confirm monthly capacity, standard and customized lead times, safety-stock policy, production-planning method, and contingency arrangements for critical operations. | Capacity plan, anonymized on-time-delivery data, production schedule, lead-time commitment, and documented business-continuity plan. | 5 = reliable delivery records and backup capacity; 3 = acceptable but limited visibility; 1 = frequent delays or unclear capacity. | 5% | — |
| Communication and Technical Support | Technical questions should receive clear responses covering tool geometry, machine compatibility, cutting parameters, inspection results, and corrective actions. | Response-time records, engineering contact details, quotation clarity, technical recommendations, and corrective-action response samples. | 5 = technically precise and responsive; 3 = adequate commercial communication; 1 = slow or nontechnical responses. | 5% | — |
| Total Weight | 100% | — | |||
When comparing chamfering cutter suppliers in China, do not judge price from one quotation alone. Request a complete cost sheet covering the cutter, coating, packaging, tooling adjustments, and delivery. A very low price may exclude inspection or suitable carbide grades. Check the cutter’s diameter, included angle, shank tolerance, and expected service life. Small differences can affect machine stability and edge quality.
Certifications need practical verification. Ask for an ISO 9001 certificate, material certificates, and recent inspection records. Confirm that the documents match the actual factory and production address. Request test data for runout, hardness, coating thickness, and dimensional accuracy. A certificate looks useful, but it proves little without traceable records. Sample testing matters more. Use the cutter on your own material and compare burrs, surface finish, and cutting noise.
Service quality often reveals the supplier’s real experience. Ask how technical staff select geometry for stainless steel, aluminum, hardened steel, or cast iron. Confirm response times, sample policies, replacement procedures, and support after delivery. Clear answers are valuable. Vague promises are not. I have seen buyers focus too heavily on unit price and overlook delayed samples or inconsistent batches. That mistake is easy to repeat. A reliable supplier should provide realistic lead times, written specifications, and inspection photos before shipment. Even then, keep your own incoming inspection records. Suppliers can improve, but buyers must verify.
Choosing a chamfering cutter supplier in China requires more than comparing prices. Verify samples against your actual material, spindle speed, and edge geometry. Request at least three pieces from one production batch. Measure diameter, chamfer angle, corner radius, coating, and runout with calibrated tools. A sample that performs well once may still hide process variation.
Ask for a test report showing cutting speed, feed rate, tool life, and surface roughness. ISO 4287 defines surface-texture parameters, while ISO 2768 supports general dimensional tolerances. These references make supplier claims easier to check. Keep the failed sample, too. It can reveal poor edge preparation or unsuitable carbide grade.
Customization should be documented, not promised verbally. Require a controlled drawing, revision number, tolerances, coating specification, minimum order quantity, and delivery schedule. Confirm whether the supplier can provide first-article inspection records and material certificates. The 2022 ISO Survey reported more than 1.2 million ISO 9001 certificates worldwide, but certification alone does not prove cutter consistency. That is an uncomfortable truth.
Supplier reliability appears in small details. Check batch traceability, inspection equipment, corrective-action records, and response time. Request references from comparable machining applications without demanding confidential customer information. A video call can show grinding, coating, and final inspection areas, although it cannot replace an audit. I would also place a small repeat order. Consistency matters more than one impressive sample.