Biotech, pharma, food industries equipment & plants
Choosing the right Machine Spindle is not a simple catalog decision. It affects accuracy, cycle time, surface finish, energy use, and maintenance costs. A spindle that looks powerful on paper may perform poorly during real cutting.
Dr. Scott Smith, a recognized researcher in machine-tool spindle technology, has said, “The spindle is the heart of the machine tool.” This short statement explains its importance. The spindle transfers motor power to the tool while controlling speed, torque, vibration, and heat. A mismatch can appear as chatter on an aluminum edge, burnt marks on steel, or unstable holes in a precision component.
Begin with the cutting process. Define the material, tool diameter, required speed range, torque demand, and expected duty cycle. High-speed machining may require a compact electric spindle with excellent balancing and cooling. Heavy roughing usually needs stronger low-speed torque. Taper type matters too. HSK and BT systems offer different gripping behavior and tool-change characteristics.
Do not ignore the machine’s structure. A rigid spindle cannot correct a weak column, poor bearings, or an unstable foundation. Cooling is also easy to underestimate. A spindle running at 24,000 rpm generates heat, even during apparently light work.
There is no perfect spindle. That is the uncomfortable part. Buyers sometimes focus on maximum rpm and overlook torque curves, bearing life, service access, and replacement time. Compare measured performance, not attractive numbers. Speak with the manufacturer, inspect test data, and consider how the spindle will behave after years of production.
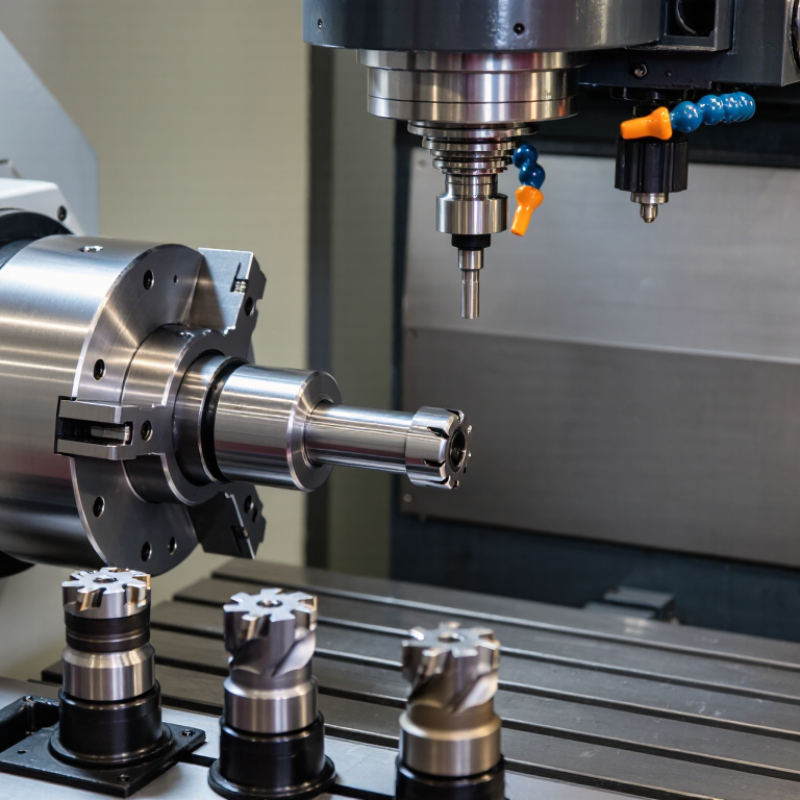
A machine spindle is the rotating heart of a machining system. It holds the cutting tool and transfers power to the workpiece. Its speed, torque, stiffness, and runout directly affect accuracy and surface quality. High-speed spindles suit small cutters and aluminum, while high-torque models handle deep cuts in steel. The right choice depends on material, tool diameter, cutting depth, and production volume.
In practical setup work, I have seen operators choose speed before checking torque. That assumption was wrong. A spindle may reach impressive revolutions per minute but still struggle during heavy milling. Check the continuous power rating, not only the peak value. Bearing design, cooling method, tool-holding accuracy, and duty cycle also matter. A warm spindle can gradually lose precision, especially during long machining cycles. Specifications help, but real cutting tests reveal more.
Tips: Match spindle torque with your heaviest regular cut. Confirm the taper fits your tooling system. Measure runout near the tool nose, not only at the spindle body. Leave thermal warm-up time before precision work. Review maintenance access, because neglected lubrication and contamination shorten spindle life. I would also record vibration, sound, and temperature during trial runs. These details often expose problems that a catalog does not show.
How to Choose the Right Machine Spindle?
Define the Required Speed, Torque, and Power
Choosing a spindle starts with the cutting job, not the spindle catalogue. Identify the material, tool diameter, cutting speed, and feed rate. A small aluminum cutter may need high speed but modest torque. A large steel cutter usually demands the opposite. Measure the real cutting conditions whenever possible. Estimates can hide costly mistakes.
Cutting speed helps determine spindle speed: RPM equals cutting speed divided by tool circumference. For a 10 mm cutter running at 150 meters per minute, the required speed is about 4,775 RPM. Torque depends on cutting resistance and tool size. Power connects both values through P = T × ω. A spindle can reach the target RPM yet stall under load. That is a common selection error.
Check continuous power, peak power, and duty cycle separately. A spindle rated for short bursts may overheat during an eight-hour production shift. Leave practical capacity for tool wear, interrupted cuts, and imperfect setup. More power is not always better; excess capacity can increase cost, heat, and energy use. I have seen projects focus on maximum RPM while ignoring low-speed torque. That shortcut looked efficient. It was not. Test the spindle with the actual tool, workpiece, and coolant conditions before final approval.
Match the spindle design to the material and machining task. Aluminum often needs high speed, efficient chip evacuation, and reliable cooling. Steel usually demands stronger torque at moderate speeds. Hardened alloys require rigidity, stable bearings, and controlled thermal growth. A spindle rated only by maximum rpm can mislead. Cutting load matters more.
The U.S. Department of Energy’s 2022 Bandwidth Study estimates that motor-driven systems consume about 68% of manufacturing electricity. Spindle efficiency therefore affects both machining cost and factory energy use. Select power from the actual cutting range, not the nameplate peak. A 20,000-rpm spindle may perform poorly during heavy steel roughing if torque falls sharply below 6,000 rpm. Small details matter.
Check the tool interface, bearing arrangement, cooling method, and duty cycle. ISO 230-2 testing emphasizes positioning accuracy and repeatability, but those values do not replace cutting trials. In practice, a rigid spindle with lower speed can produce cleaner titanium surfaces than a faster, flexible unit. I have seen specifications look impressive while vibration appeared at the tool tip. That is worth questioning. Short test cuts should measure sound, temperature, power draw, and surface finish. Also review maintenance access and repair intervals. A technically perfect spindle becomes a poor choice when cooling lines clog or preload cannot be checked. Your material, cutter diameter, and removal rate should define the spindle—not marketing numbers.
Accuracy begins with measured behavior, not a catalog promise.
Check radial and axial runout at the tool nose, then review accuracy under operating temperature. ISO 230-2 defines methods for testing positioning accuracy, while ISO 230-3 addresses thermal effects.
A spindle may hold excellent cold readings and drift after two hours of cutting. That detail matters.
Record warm-up time, speed range, vibration, and surface-finish results using your actual tooling.
High-speed aluminum cutting creates different heat than slow, heavy steel milling. Review oil-air or liquid-cooling capacity, temperature stability, and alarm response.
The U.S. Department of Energy reports that compressed-air leaks can waste 20–30% of compressor output. Poor air maintenance can therefore affect tool changes and operating costs.
Bigger cooling capacity is not always better; excessive flow may hide a thermal problem rather than solve it.
Measure clamping force, balance quality, taper condition, and repeatability after repeated changes. A rigid holder cannot correct a damaged taper.
It sounds obvious, but shops still overlook it.
Maintenance planning should include lubrication intervals, filter replacement, bearing monitoring, and accessible inspection points.
Plant Engineering’s 2023 Maintenance Study reported that 82% of surveyed facilities experienced unplanned downtime within three years. That statistic should influence spindle selection.
I would rather choose a slightly slower spindle with clear service access than chase maximum speed and discover expensive downtime later.
Choosing a machine spindle is a cost decision, not merely a speed decision. In real machining, the cheapest quote can become expensive after tooling changes, downtime, and control integration. Compare purchase price, installation, drive requirements, cooling equipment, and replacement bearings. Estimate total cost per productive hour, not invoice value alone. Keep assumptions visible.
Compatibility starts with the interface: taper standard, flange dimensions, encoder feedback, voltage, maximum speed, torque curve, and coolant arrangement. The International Federation of Robotics’ World Robotics 2024 report recorded 541,302 industrial robot installations worldwide in 2023. This expansion makes signal compatibility and service support more important, even for a standalone machine. ISO 230-2 testing can verify positioning performance, but it cannot guarantee cutting stability.
Service life depends on heat, imbalance, contamination, duty cycle, and operator habits. Ask for bearing ratings, runout limits, lubrication intervals, repair procedures, and documented failure data. A high-speed spindle may cut aluminum beautifully, then struggle with heavy steel cuts. That is an easy mistake. Select by the actual torque curve, not headline rpm. Market reports often show growth, but rarely reveal downtime in your workshop. Measure vibration and temperature during representative jobs, then revise the choice when evidence disagrees with the first estimate.